Choosing between PVDF, electrophoretic coating, powder coating and wet paint requires more than comparing product labels or price per square metre. By the end, you will be able to match the coating system to the substrate, Mumbai exposure, geometry, appearance and evidence required before requesting comparable quotations.
Key takeaways
- Choose E-coat for immersed conductive parts needing uniform coverage.
- Specify pretreatment, film build, cure temperature and test evidence in writing.
- Match the coating system to Mumbai’s humidity, salt exposure and metal substrate.
- Compare repair requirements, rejects and service life—not coating price alone.
What “electro coating” means, and how it compares with PVDF
Electro coating for metal products means electrophoretic deposition, or E-coat: immerse a conductive metal part in a paint bath and use an electric field to deposit the coating. It is not electrostatic powder spraying, which charges dry powder and sprays it onto a grounded part.
Cathodic E-coat is commonly chosen for corrosion protection because the workpiece is less likely to dissolve than in anodic E-coat. Epoxy baths resist corrosion and chemicals but usually need a UV-resistant topcoat outdoors; acrylic baths weather better, but do not automatically match epoxy’s corrosion performance.
| Option | Corrosion protection | UV, build, edges and appearance | Speed, repair and cost drivers |
|---|---|---|---|
| PVDF | Strong when the full primer/topcoat system is qualified | Excellent colour and gloss retention; thin-to-medium film; spray coverage depends on access; smooth architectural finish | Fast line application; local repairs are difficult to colour-match; resin, pretreatment, masking and curing drive cost |
| E-coat | Excellent primer protection, especially cathodic epoxy | Uniform thin film reaches recesses better than spraying; limited at Faraday cages, trapped air, poor drainage and sharp edges; usually needs a topcoat outdoors | High-throughput immersion; repairs require approved systems; bath control, tanks and curing drive cost |
| Super-durable powder | Strong with correct pretreatment and specification | Thicker film, good UV retention; edges and cavities depend on spraying; textured or smooth finish | Fast; chips permit local repair; powder recovery, colour changeovers and oven capacity drive cost |
| Wet paint | Depends heavily on primer and application | Broad appearance choices; variable thickness and edge coverage; UV retention depends on resin | Flexible for small batches; slower drying and more labour increase cost |
E-coat and PVDF are not automatic alternatives: E-coat can be the corrosion-resistant primer, with PVDF as the exterior topcoat in a duplex system. Choose the complete system for the substrate, exposure and appearance—not the label alone.
Match the complete system to Mumbai exposure and substrate
Choose by site, not city name: classify wetness, salinity and pollutants under ISO 12944 and ISO 9223, then match the substrate and assembly. Mumbai’s monsoon, salt air, industrial fallout, standing water and intense sunlight make a marine-facing façade different from an inland factory or sheltered urban installation.
| Exposure | Main stress | System direction |
|---|---|---|
| Marine-facing exterior | Salt, UV and persistent wetting | High-performance architectural system, with drainage and dissimilar-metal isolation |
| Inland factory | Pollution and humidity, less salt | Qualify pretreatment and corrosion resistance for the actual exposure |
| Sheltered indoor part | Low UV and controlled wetting | Avoid over-specifying PVDF unless appearance or cleaning demands it |
Aluminium, galvanised steel, mild steel and stainless steel need different cleaning and conversion coatings. Pretreatment proven on mild steel does not qualify aluminium or galvanised steel; mixed-metal contact can cause galvanic corrosion where water stands. One blanket specification is poor engineering.
Do not treat PVDF as one grade. Verify binder chemistry, primer/topcoat structure and whether the architectural liquid system is marketed around 70% PVDF. For a hyper durable PVDF coating in Mumbai, request AAMA 2603, AAMA 2604 or AAMA 2605 classification with complete-system evidence.
PVDF is a poor fit for hidden indoor parts, short-life low-cost components, very small batches or severe abrasion. E-coat is unsuitable for oversized profiles, incompatible substrates or exposed decorative surfaces without a suitable UV-resistant topcoat.
Specify film build, pretreatment, cure and test evidence
Before approval, require a system dossier that links film build, pretreatment, cure and test evidence to your actual substrate and exposure.
1. For PVDF, request the resin type and binder formulation, complete primer-and-topcoat structure, dry-film thickness, gloss range, colour tolerance, pretreatment sequence, cure schedule, warranty scope and current technical data sheets. Verify claims such as “70% PVDF” rather than accepting the label alone.
2. For E-coat, record whether the process is cathodic or anodic, the bath chemistry, degreasing and conversion-coating sequence, rinses, target thickness, cure schedule, edge-coverage method and qualification results for the actual substrate. Mild-steel evidence does not qualify aluminium, galvanised steel or mixed-metal assemblies.
3. Request reports using ASTM B117 or ISO 9227 salt spray; ASTM D4587 or ISO 16474-3 accelerated weathering; ASTM D2244 colour change; ASTM D523 gloss; and ASTM D3359 or ISO 2409 adhesion. Each report must identify the laboratory, duration, panel preparation, batch, cure record, failure definition and deviations.
4. Check that stated acceptance criteria match the system, substrate, laboratory, film build and exposure condition. These methods are not interchangeable. Treat salt spray and accelerated-weathering results as screening evidence, not field-life predictions; warranty wording is not a conversion table.
If a supplier cannot provide the requested records, mark the performance claim unverified and do not approve the system.
Control the application from metal preparation through repair
Start with the part, not the coating: inspect drainage, welds, edges, cavities and internal surfaces, then design the process around access and water removal.
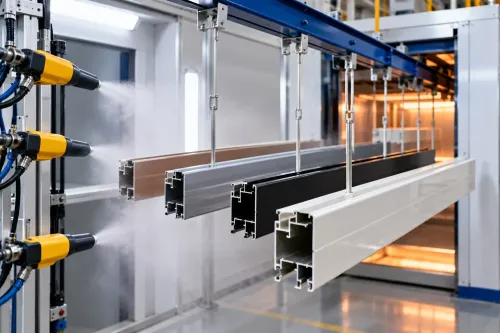
1. Degrease the substrate, rinse, apply the conversion coating specified for that metal, rinse again and dry completely. Mask threads, contact faces and areas that must remain bare; then rack the part or immerse it for E-coat. Spray PVDF or powder where the specification requires it.
2. Cure against recorded metal temperature and time, not oven-air temperature alone. Inspect dry-film thickness, colour, gloss, adhesion-related defects, pinholes, runs, racking marks and Faraday-cage zones before packing without trapping moisture.
3. Confirm feasibility before accepting the job. Profile length and part size must fit the oven; E-coat requires adequate bath-tank dimensions, line capacity and bath turnover. Batch volume, rack loading, Mumbai transport and colour changes affect queue time, masking, cleaning and lead time.
Weld spatter and sharp edges create thin coverage; radius or dress them before coating. Drill cut-outs and provide drainage for cavities, because trapped air and liquid leave bare zones. Specify access to internal surfaces and racking locations.
Store aluminium clean and dry, isolate it from steel contamination, apply protective film after inspection, and control cutting or drilling after coating. Seal exposed edges and remove chips immediately.
For scratches or chips, use an approved touch-up system only when damage is local and the warranty permits it. Strip and recoat when corrosion has spread, adhesion is lost, fading prevents a decorative match, or the repaired area no longer blends with the surrounding field.
Compare Mumbai quotations by total system cost, not coating price alone
A low rupees-per-square-metre quote can become expensive after rejects, rework and site damage. Compare the complete system, not the coating material alone.
Send every PVDF coating supplier in Mumbai the same:
- Drawing, substrate, exposure zone, indoor or outdoor placement, appearance, colour and gloss tolerance
- Required service life, warranty period, film build, pretreatment and edge preparation
- Test requirements, test evidence, batch traceability and approved touch-up method
- Minimum order, line and oven capacity, packing specification and installation-handling instructions
Cost drivers include pretreatment equipment, curing energy, masking, racking, bath maintenance and colour changeover. Add transport, rejects, rework and installation damage before choosing a durable metal coating in Mumbai.
| Compare | Ask for | Reject the quote when |
|---|---|---|
| Process | Cure records, thickness mapping and pretreatment sequence | It gives only a material price |
| Performance | AAMA class, test report, substrate and acceptance criteria | “Durable” has no class or evidence |
| Delivery | Capacity, minimum order, packing and repair method | Exclusions are unclear |
Common mistakes include treating ASTM B117 salt-spray hours as outdoor life, skipping pretreatment, specifying colour without gloss tolerance, coating wet or contaminated metal, and creating water traps in the design.
AMECO World of Coatings is one Mumbai option to question about the proposed process, technical data sheet, cure records, test reports, traceability, capacity and repair method; do not assume electro-coating capability, certification, warranty or performance without project-specific documents.
Related products
 | Products as well as projects exposed to very harsh climatic and industrial conditions require extremely durable range of coatings. View product → |
 | Ameco powder coating effect on metals is a safer and better alternative to conventional acrylic and polymer wet spray painting. View product → |
Frequently asked questions
What is electro coating for metal products?
Electro coating, or E-coat, immerses a conductive metal part in a paint bath and uses an electric field to deposit the coating. It differs from electrostatic powder spraying, which applies charged dry powder to a grounded part.
How does PVDF compare with E-coat?
PVDF is a high-performance architectural finish applied as a liquid coating system, while E-coat is an immersion process that provides consistent coverage on conductive parts, including recessed areas. Compare the complete system, including pretreatment, film build, cure and testing.
How should you specify a coating system for Mumbai exposure?
Specify the metal substrate, exposure conditions, pretreatment, coating chemistry, film-build range, cure schedule and required test evidence. Include humidity, coastal salt exposure and the product’s repair conditions in the specification.
What should you compare in Mumbai coating quotations?
Compare pretreatment, coating material, application, curing, inspection, rejection rates, repair work and expected service life. A lower coating price can become more expensive when the quotation excludes preparation, testing or field repairs.
Keywords